
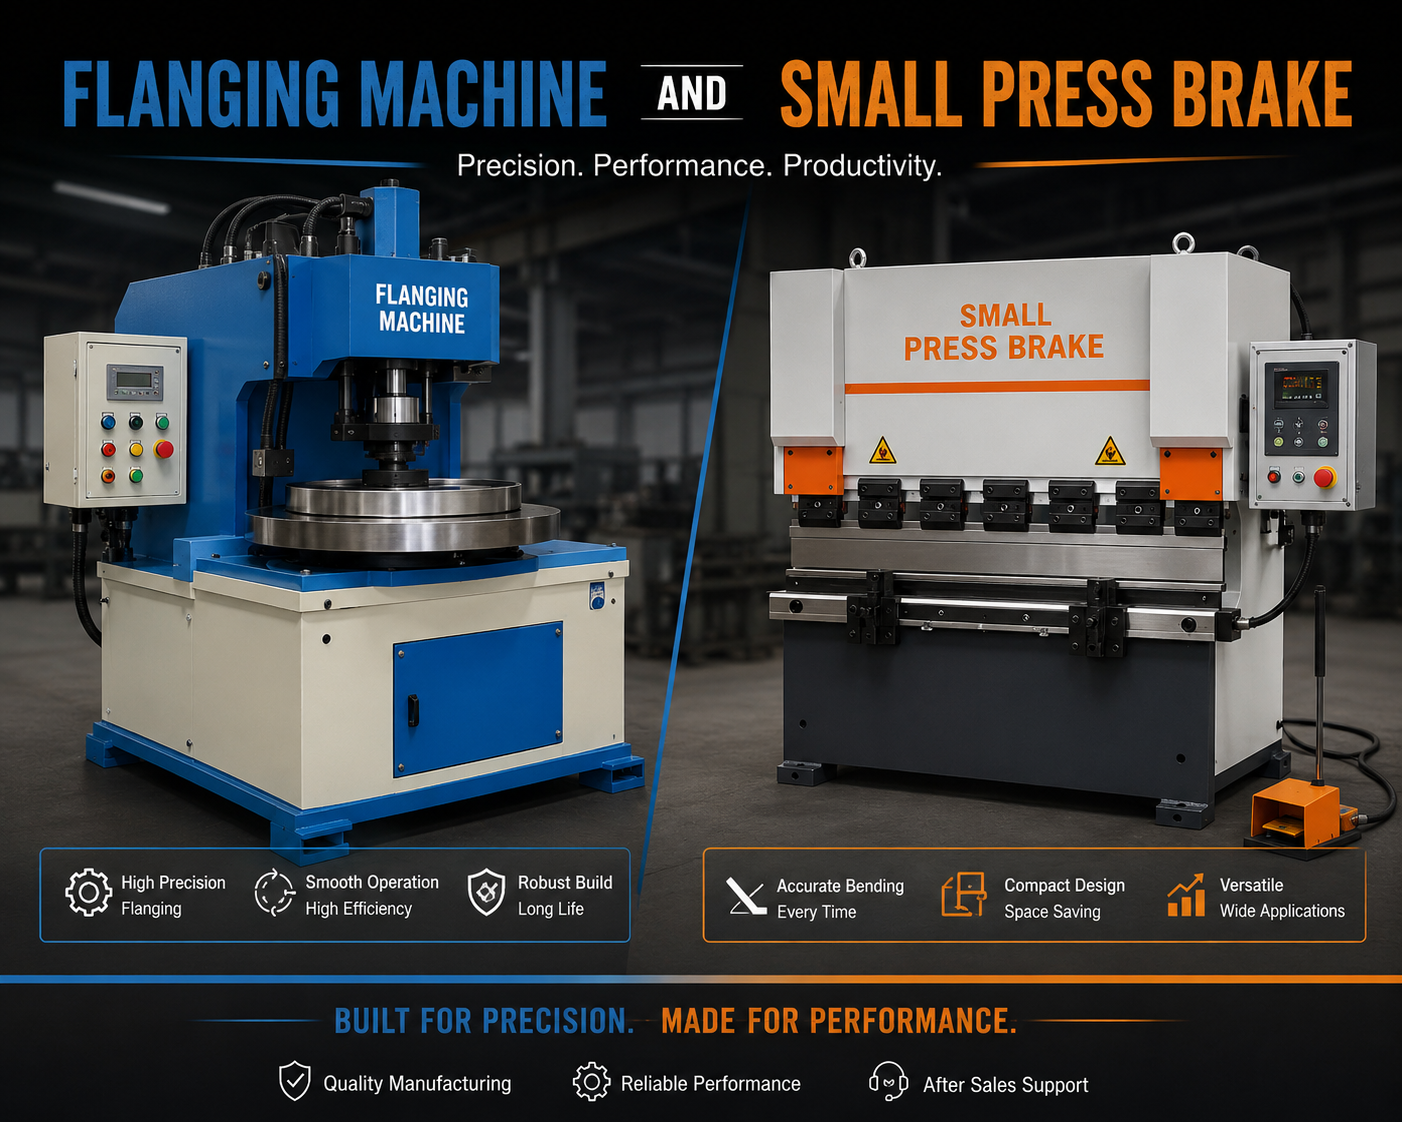
Among the most useful solutions are the flanging machine and small press brake. Both machines help manufacturers shape metal efficiently, but their functions, working principles, applications, and tooling requirements are different.
A flanging machine is mainly designed to form edges, rims, or flanges on metal parts, while a small press brake is used to create controlled bends along straight lines. Understanding these differences helps workshops select suitable machinery, reduce production errors, and achieve better finished components.
A flanging machine is specialized metal-forming equipment used to turn the edge of a metal component inward or outward. The formed edge may improve strength, provide a joining surface, increase rigidity, or prepare the component for welding and assembly.
Flanging is commonly required in industries manufacturing round, cylindrical, curved, or fabricated metal components.
The machine applies controlled forming pressure through specially designed tooling or rollers. Instead of making one aggressive bend, many flanging processes progressively form the material to minimize distortion.
Flanges perform both structural and functional roles. A properly created flange can strengthen an otherwise flexible sheet metal component.
Key advantages include:
When repetitive flange production is required, using a dedicated flanging machine can provide better consistency than manual methods.
Not every component requires the same flange geometry.
Straight flanging forms a controlled edge along a straight workpiece. It may be required for panels, covers, enclosures, and fabricated sections.
Circular flanging is often used for tanks, ducting, drums, vessels, and round components.
An internal flange is formed toward the inside of the component, while an external flange extends outward. Machine tooling should be selected according to the desired direction and radius.
A small press brake is a compact sheet metal bending machine developed for smaller components and moderate working lengths. It offers many functions of larger press brakes while requiring less floor space.
The machine uses an upper punch and lower die. As the punch moves downward, the sheet metal is pushed into the die opening and forms the required bend.
Small press brakes are especially valuable for job shops that manufacture multiple component designs in relatively small quantities.
The small press brake is popular because it combines flexibility with compact construction.
Important benefits include:
Modern machines may include digital displays, programmable controls, CNC backgauges, and multiple-axis positioning.
| Parameter | Flanging Machine | Small Press Brake |
| Primary operation | Forming metal edges | Bending sheet metal |
| Typical shape | Flanges and rims | Angles and profiles |
| Main tooling | Rollers or forming dies | Punch and die |
| Suitable work | Circular and edge forming | Straight-line bending |
| Production style | Specialized | Highly flexible |
| Typical users | Tank and duct manufacturers | General fabrication shops |
| Automation options | Manual, hydraulic, CNC | Manual, hydraulic, CNC |
The choice should depend on the component rather than simply comparing machine size or price.
A flanging machine can be found across industries where shaped sheet metal components are manufactured.
Applications include:
High repeatability is particularly important when multiple parts must fit together during later assembly.
A small press brake can produce many component types using suitable tooling.
Common examples include:
Because tooling can be changed, the machine can move from one product design to another relatively quickly.
Selecting the right machine requires more than checking maximum material thickness.
Important considerations include:
Mild steel, stainless steel, aluminum, copper, and other alloys behave differently during forming.
For circular components, both minimum and maximum supported diameter should be checked.
Required flange width, radius, direction, and final angle influence machine selection.
Manufacturers producing hundreds of identical parts may benefit from hydraulic or automated controls, while smaller workshops may prefer simpler equipment.
Before purchasing a small press brake, manufacturers should evaluate several technical parameters.
The working length must accommodate the widest component expected in production.
Required force changes according to material strength, thickness, bend length, and die opening.
A reliable backgauge helps control flange dimensions and improves repeatability.
A machine supporting widely available tooling can offer better long-term flexibility.
Machine quality alone does not guarantee accurate production. Operators should also maintain correct setup practices.
For consistent results:
Preventive maintenance also reduces unexpected downtime.
A flanging machine forms controlled edges or rims on metal sheets and fabricated components.
Yes. Many designs are developed specifically for circular and cylindrical components.
A small press brake is a compact machine used to bend sheet metal through a punch-and-die system.
Common materials include mild steel, stainless steel, aluminum, brass, and copper, depending on machine capacity.
Not completely. Each machine is optimized for different forming operations.
CNC is not essential for basic jobs, but it improves repeatability and productivity for more complex production.
Possible reasons include incorrect tooling, poor alignment, material variation, springback, and incorrect machine settings.
Tool geometry determines bend radius, flange shape, dimensional accuracy, and surface quality.
Yes. Compact manual and powered models are available for lower-volume manufacturing.
Regular cleaning, lubrication, alignment inspections, tooling maintenance, and operation within rated capacity help extend service life.
A small press brake is usually more suitable because brackets mainly require accurate straight bends.
A flanging machine is commonly preferred for producing edge flanges on circular tank and vessel components.