
Sheet-metal production is moving toward leaner manufacturing cells as fabricators look for ways to reduce material movement, shorten setup cycles, handle smaller batches, and use factory space more effectively. Rather than organizing every job around large centralized equipment, manufacturers are increasingly considering dedicated machines positioned closer to the operations where they are needed.
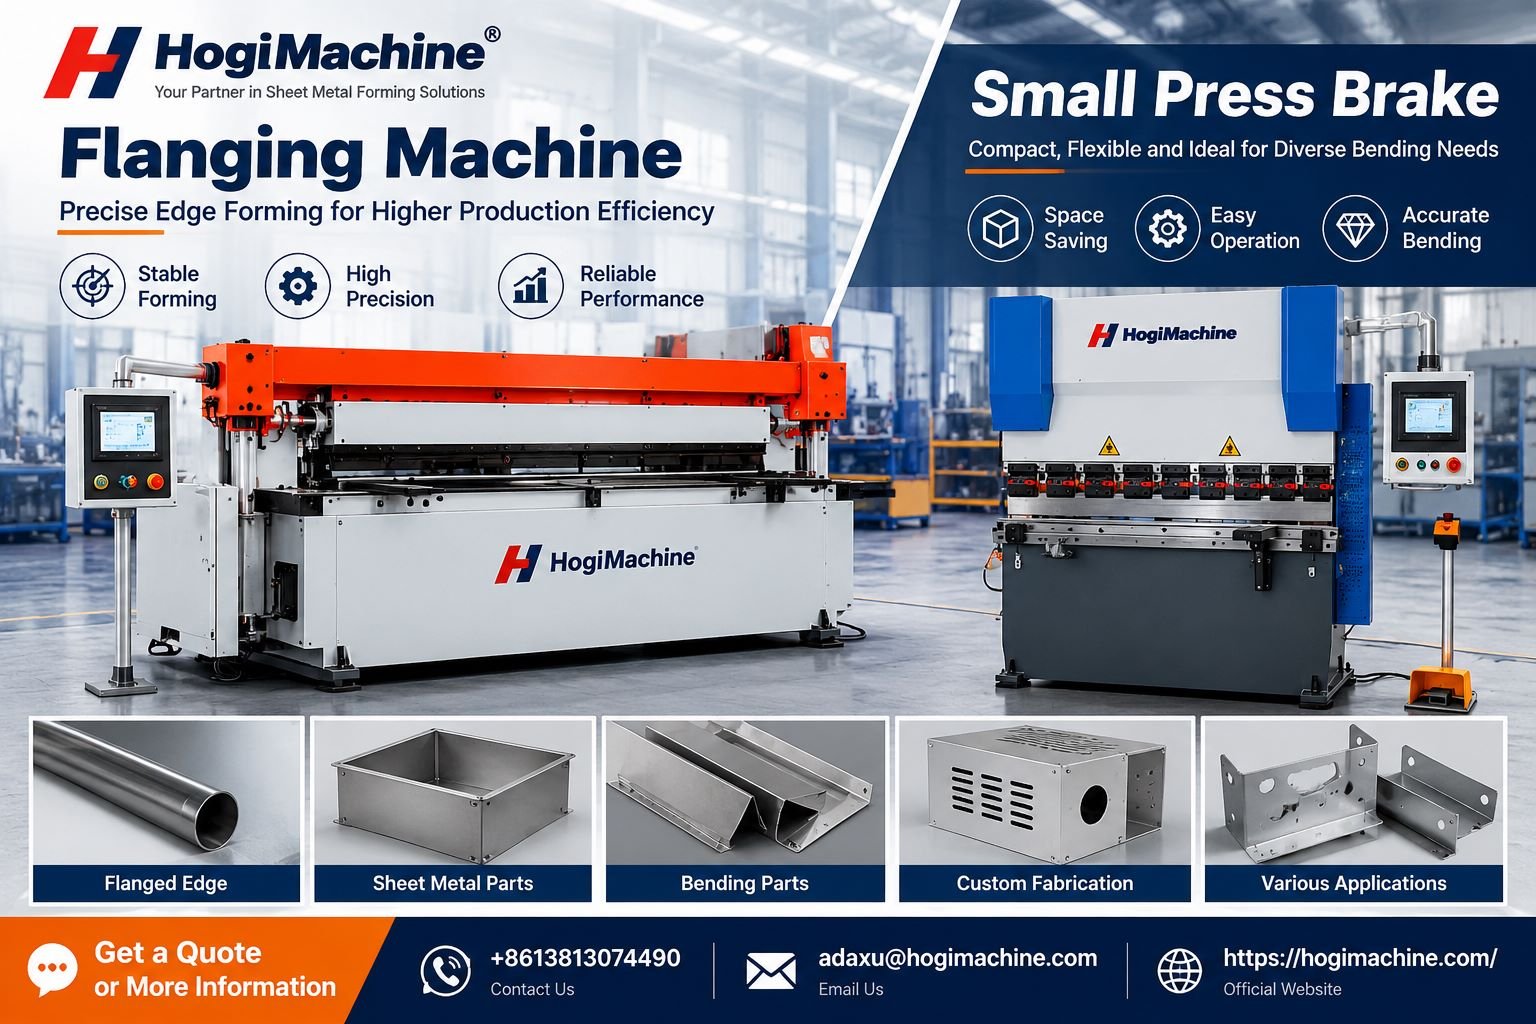
This development is creating new opportunities for the Flanging machine in specialized edge-forming work and the small press brake in compact bending applications. Together, these technologies reflect a broader shift toward right-sized equipment, where machine capability is matched closely to the component instead of automatically choosing the largest available system.
Conventional sheet-metal factories may separate cutting, bending, forming, welding, and assembly into different areas.
While this arrangement works for many operations, excessive movement between departments can add handling time, particularly for small components.
A manufacturing cell groups complementary processes where practical.
For components requiring repeated edge forming, positioning a Flanging machine within an appropriate production flow can reduce unnecessary routing and help operators maintain a more predictable sequence.
The objective is not simply faster machine operation. It is a shorter and more efficient journey from raw material to finished component.
A flange may appear to be a relatively simple feature, but its geometry can influence assembly and final product performance.
Flanges may be used to strengthen edges, provide joining surfaces, locate components, or support subsequent fabrication.
A dedicated Flanging machine can help standardize this operation when flanged components are manufactured regularly.
Before production begins, teams should define the required geometry, material, thickness, workpiece dimensions, and acceptance requirements.
Clear process planning reduces dependence on improvised forming methods and gives operators a consistent production target.
Large press brakes are essential when components require substantial forming capacity or longer working dimensions. However, using a large machine for every small bracket or compact panel may not always represent the best allocation of resources.
A small press brake provides an alternative for jobs that fall comfortably within its capabilities.
Suitable smaller components can be routed to the compact machine, allowing larger equipment to remain available for work that genuinely requires greater capacity.
This type of capacity segmentation can improve scheduling in workshops processing a diverse range of components.
A machine can bend or form a component quickly while still spending significant time between jobs.
Tool changes, material preparation, program selection, measurement, and first-piece verification can all contribute to setup time.
For short production runs, these activities become particularly important because setup represents a larger percentage of total job time.
Manufacturers using a small press brake can improve productivity by organizing frequently required tooling, maintaining controlled job information, and developing clear setup procedures.
Reducing avoidable preparation time can increase usable manufacturing capacity without increasing machine speed.
The beginning of a production run deserves careful attention.
Before completing an entire batch, manufacturers can inspect the first acceptable component against the required dimensions or geometry.
This provides an opportunity to identify setup problems before additional material and labor are committed.
First-piece verification can be useful for both Flanging machine operations and press brake work.
The inspection method should match the actual component requirements. Critical features may justify closer attention than characteristics with little effect on assembly or function.
Excessive work-in-progress can occupy valuable floor space and make production priorities difficult to see.
If components are formed in large batches simply because machines are located far apart or setups are inconvenient, material may spend significant time waiting between operations.
Right-sized equipment can support smaller, more controlled batches where this approach suits production needs.
A small press brake located within a suitable fabrication workflow can allow compact components to progress to the next operation without waiting for availability on larger equipment.
This is one reason compact machinery can create value beyond its physical footprint.
Productivity should never be separated from safe machine operation.
Sheet-metal forming involves moving components, tooling, pinch points, and substantial forming forces. Appropriate safeguards, operating procedures, training, and equipment-specific instructions are therefore essential.
Buyers evaluating a Flanging machine should consider how operators load, support, form, and remove components.
The same principle applies when selecting compact bending equipment.
Manufacturers should follow applicable safety requirements and the equipment manufacturer’s instructions for installation, operation, and maintenance.
Scratches, dents, and deformation do not always originate during the forming cycle.
Components can be damaged while being stacked, transported, stored, or moved between workstations.
This is particularly relevant when products have visible surfaces or need to fit accurately during assembly.
Manufacturers can evaluate trays, racks, worktables, protective surfaces, and component stacking according to their production needs.
By treating material handling as part of the manufacturing process, workshops can help preserve the quality created by their forming equipment.
Factories increasingly consider operating expenses when purchasing machinery.
However, energy efficiency should be evaluated together with production requirements rather than as an isolated specification.
The most appropriate equipment is one that can safely and effectively perform the required work while supporting the desired production strategy.
Using a small press brake for appropriately sized jobs can be part of a right-sized manufacturing approach, but machine selection should always begin with forming requirements and rated capability.
Maintenance becomes easier to manage when information is documented.
Recording routine inspections, service activities, tooling condition, and recurring technical issues can help teams understand machine history.
If an abnormal condition appears repeatedly, previous records may provide useful context for troubleshooting.
For a frequently used Flanging machine, systematic records can also support maintenance scheduling and production planning.
The same principle applies to compact bending equipment and other fabrication machinery.
A Flanging machine is used to create a formed flange, lip, or edge on a metal workpiece for purposes such as assembly, reinforcement, positioning, or joining.
A small press brake is compact sheet-metal bending equipment intended for components that fit within its specified working dimensions and forming capacity.
Manufacturing cells can reduce unnecessary component movement and waiting by placing related production operations closer together where practical.
Not universally. Machine choice depends on component size, material, thickness, bend length, required force, tooling, and other production requirements.
It is the verification of an initial production component before continuing with a larger batch, helping identify setup or quality issues early.
In short production runs, setup can represent a significant portion of total manufacturing time, making efficient preparation valuable.
Material type, thickness, component geometry, flange requirements, production volume, handling, machine capability, and technical support should all be considered.
Clearly identified and properly stored tooling can reduce search and preparation time while supporting more consistent setups.
Poor handling can introduce scratches, dents, or deformation even when the forming operation itself is correct.
Yes. Planned inspection and servicing can help identify developing problems and reduce the risk of unexpected production interruptions.
Metal Forming Machinery Enquiries
Contact: +86 138 1307 4490
Email: adaxu@hogimachine.com
Official Website: hogimachine.com