
Across food processing, chemical manufacturing, pharmaceuticals, and speciality material industries, the movement of raw materials between processing stages is an important engineering consideration.
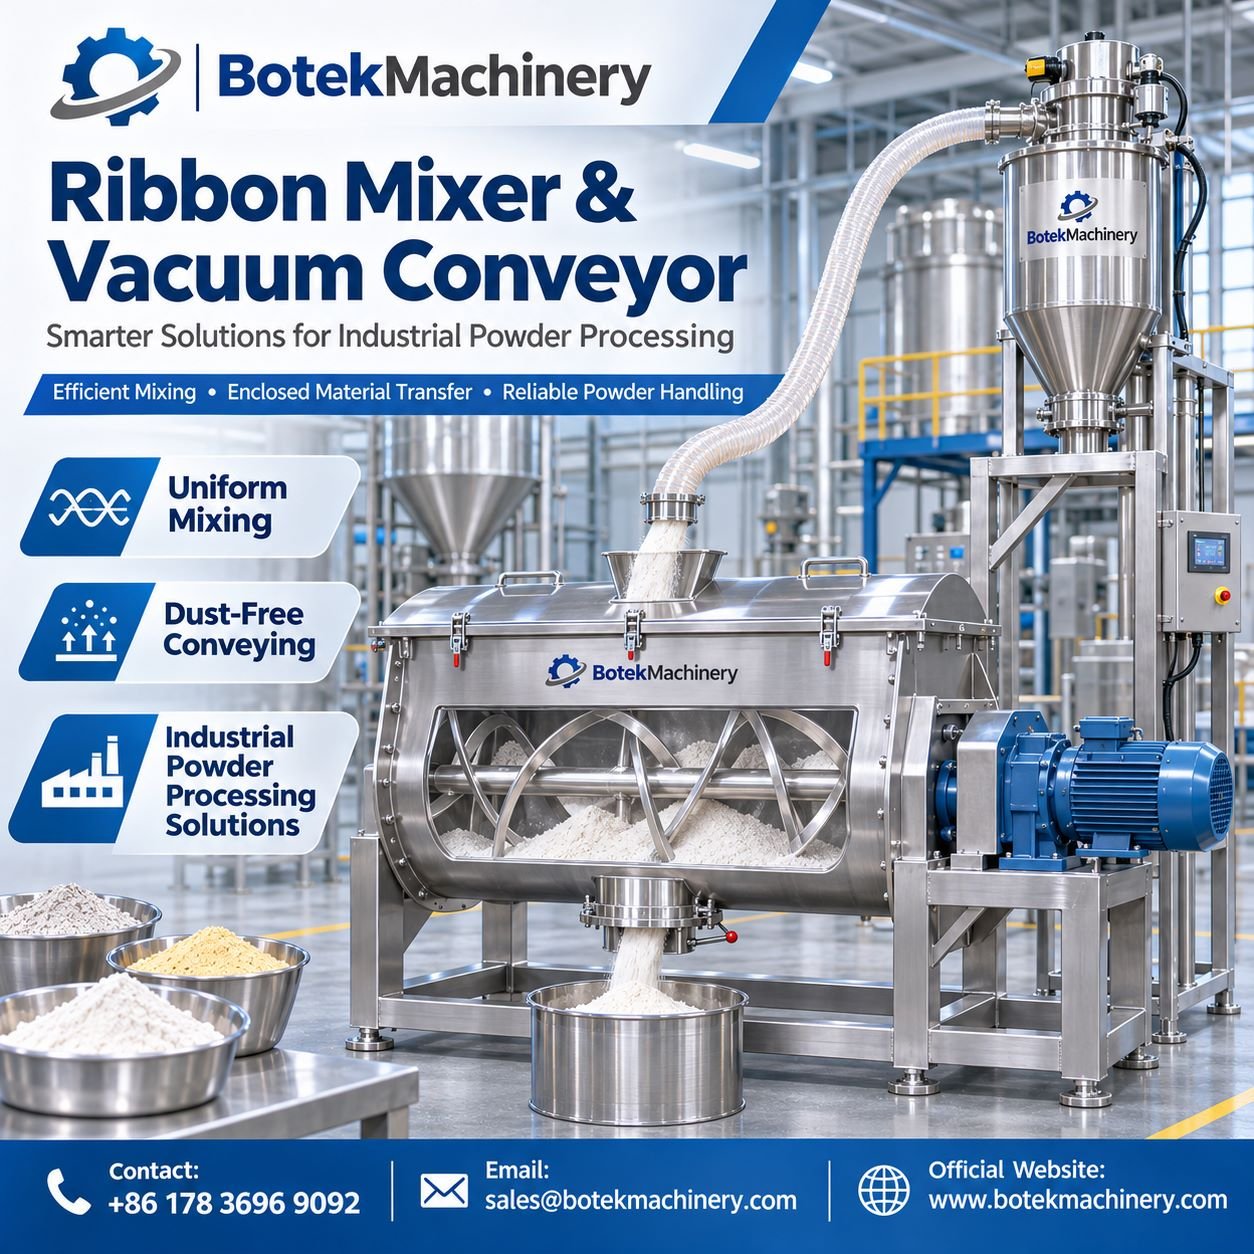
A ribbon mixer supports the blending of suitable powders, granules, and other compatible materials through a mechanically driven mixing system.
Meanwhile, a vacuum conveyor transports suitable bulk materials through an enclosed conveying arrangement using a pressure difference.
When correctly integrated, these technologies can help manufacturers organise material transfer, reduce unnecessary manual handling, and improve batch processing workflows.
For production managers and industrial equipment buyers, understanding how mixing and conveying equipment work together can support more informed manufacturing decisions.
Powder processing involves more than combining ingredients inside a mixing vessel.
Raw materials must be received, identified, transferred, measured, processed, and discharged according to production requirements.
Manual handling can introduce operational challenges, including material spillage, inconsistent transfer practices, and additional cleaning requirements.
Automated conveying systems may help address some of these concerns when properly designed.
This system-level approach encourages manufacturers to evaluate material handling and mixing as connected operations.
A ribbon mixer is an industrial mixing machine commonly used to blend suitable dry powders, granules, and certain other materials.
It typically consists of a horizontal mixing chamber containing a rotating shaft fitted with helical ribbon elements.
The rotating ribbons move materials through the vessel, promoting redistribution and mixing.
Mixing performance depends on ingredient properties, equipment construction, operating conditions, and the required blending outcome.
A vacuum conveyor is material handling equipment that uses a pressure difference to transport suitable powders or granules through a conveying pipeline.
A typical system may include a vacuum source, receiving vessel, filter arrangement, transfer pipeline, and discharge mechanism.
Material is drawn from a designated collection point towards the receiving equipment.
The conveying cycle and discharge arrangement depend on the system design.
Vacuum conveying can support material transfer between storage containers, feeding stations, processing machines, and packaging equipment.
However, conveying performance varies according to material density, particle characteristics, pipeline configuration, and equipment capacity.
A carefully designed production line can combine enclosed material transfer with mechanical blending.
Raw materials may be collected from suitable containers and conveyed towards a receiving hopper or mixing system.
The conveyor delivers the material to the designated processing point.
The mixer then blends the ingredients according to an established production procedure.
After mixing, the finished material can be discharged for further processing or packaging.
The arrangement may reduce certain manual handling activities.
However, automated transfer does not automatically guarantee accurate ingredient dosing. Appropriate weighing, feeding, and control equipment may still be required.
Consistent product composition begins with correct ingredient quantities.
Even an effective mixer cannot compensate for an incorrect formulation.
This makes material identification and dosing important parts of production planning.
Manufacturers should distinguish between transferring a material and measuring its quantity.
A conveying system moves material, while suitable weighing or metering equipment verifies the amount delivered.
Connecting these functions through appropriate process controls can support more consistent production practices.
Powder transfer can create housekeeping and exposure concerns when materials are handled openly.
An appropriately engineered vacuum conveying arrangement may reduce dust release at certain transfer points.
Enclosed equipment can also help limit unnecessary contact between materials and the surrounding environment.
Nevertheless, enclosed conveying does not eliminate all contamination or occupational exposure risks.
The system may require filtration, suitable seals, maintenance procedures, and additional dust control measures.
For combustible powders, appropriate hazard assessments and engineered protection systems are essential.
Manufacturers often process multiple formulations using shared production equipment.
This can create challenges involving material changeovers, equipment cleaning, and batch identification.
A ribbon mixer may require specific cleaning procedures depending on its internal construction and the processed materials.
A vacuum conveyor also requires consideration of pipeline cleaning, filter maintenance, and residual material.
Equipment accessibility and cleanability should therefore be evaluated before purchase.
Production flexibility depends on the complete system design rather than the capabilities of one machine alone.
| Processing Factor | Ribbon Mixer | Vacuum Conveyor |
| Primary Function | Blending compatible materials | Transferring suitable bulk materials |
| Operating Principle | Mechanical ribbon agitation | Pressure-difference conveying |
| Main Production Stage | Mixing | Material transfer |
| Important Consideration | Blend uniformity | Conveying suitability |
| Typical Supporting Equipment | Feeders and discharge systems | Filters, receivers, and pipelines |
| Quality Objective | Consistent ingredient distribution | Controlled material movement |
The technologies perform separate functions but can complement each other in suitable processing systems.
Manufacturers should assess equipment using relevant production indicators.
For mixing operations, important measurements may include blend uniformity, batch consistency, material discharge behaviour, and product quality.
For conveying systems, useful observations include transfer performance, residual material, filtration condition, and operational reliability.
A good evaluation also considers cleaning requirements and equipment accessibility.
Manufacturers should conduct representative trials using actual or suitably comparable materials.
Such testing can reveal limitations that may not be apparent from general product specifications.
Before choosing equipment, purchasing teams should establish the production requirements.
Important factors include:
Technical evaluations should reflect the intended application and relevant industry requirements.
1. What is a ribbon mixer used for?
A ribbon mixer is used to blend suitable powders, granules, and certain other materials through mechanical agitation inside a horizontal mixing chamber.
2. What is the purpose of a vacuum conveyor?
A vacuum conveyor transports suitable bulk materials through a pipeline using a pressure difference, supporting enclosed material handling operations.
3. Can a vacuum conveyor feed a ribbon mixer?
Yes. Suitable systems can be integrated, although feeding accuracy, discharge arrangements, and equipment compatibility must be evaluated.
4. Does vacuum conveying completely eliminate dust exposure?
No. It may reduce dust release when correctly engineered, but filtration, maintenance, cleaning, and appropriate safety controls remain necessary.
5. Which industries use ribbon mixers and vacuum conveyors?
Depending on equipment design and material compatibility, applications can include food processing, chemical manufacturing, pharmaceuticals, speciality powders, and other bulk material industries.
Department: Industrial Mixing and Material Handling Equipment Enquiries
Contact: +86 178 3696 9092
Email: sales@botekmachinery.com
Official Website: https://www.botekmachinery.com/